Global buyers are entering a more demanding phase of automation engineering. Machines must do more than repeat tasks. They must connect with people, software, sensors, and changing production goals. A robotic arm may now share data with a warehouse system while operators monitor energy use from another country.
Joseph Engelberger, widely regarded as the father of industrial robotics, said, “The first step in automation is to start.” His words remain practical. Yet starting is no longer enough. Buyers must ask harder questions about cybersecurity, maintenance skills, integration costs, data ownership, and supplier support.
This overview examines the 2026 trends shaping automation engineering across global markets. Artificial intelligence, digital twins, collaborative robots, industrial edge computing, and low-carbon production will influence purchasing decisions. However, technology alone will not guarantee results. A brilliant system can still fail when spare parts arrive slowly or workers receive weak training.
Look closely.
Reliable procurement will depend on measurable performance, transparent standards, and realistic deployment plans. Buyers should compare cycle times, energy consumption, safety functions, software compatibility, and total ownership costs. Regional regulations and workforce conditions also deserve attention. They can change the business case quickly.
Some forecasts may prove wrong. That is worth admitting. Automation adoption is uneven, and smaller manufacturers may need simpler solutions before advanced platforms. The strongest strategy may not be the most futuristic one. It may be the system that operators understand, maintain, and improve every day.
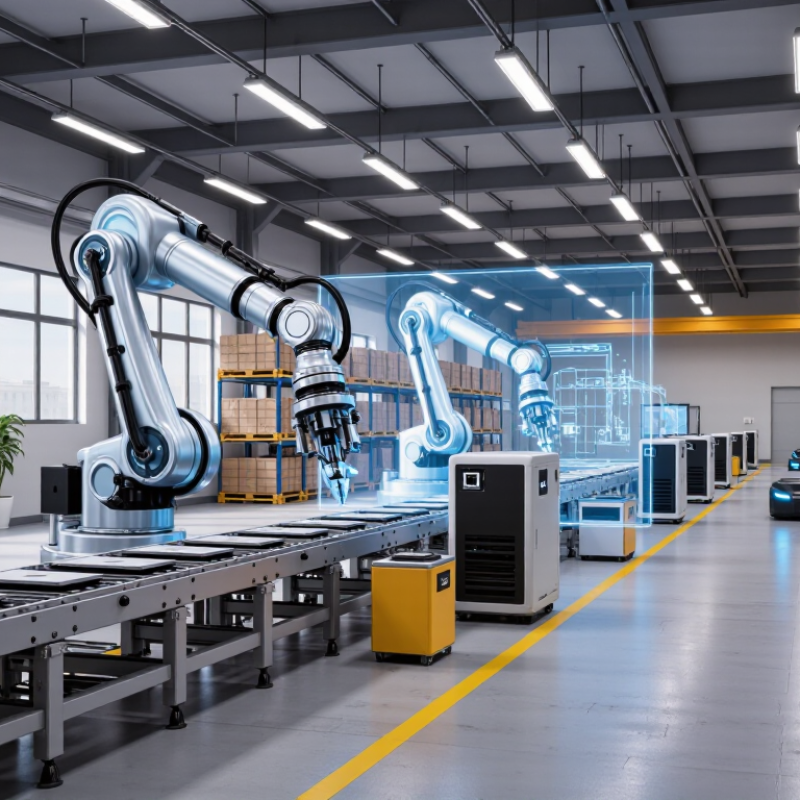
In 2026, automation engineering means designing and integrating machines, controls, software, and data systems to perform work reliably. It covers more than installing a robot. Engineers assess the task, select sensors and actuators, program control logic, and connect equipment with production systems. They also consider operator access, maintenance, energy use, and safe machine behavior. The scope can include one packaging cell or an entire facility. It depends on the production goal.
For global buyers, a useful definition includes the full equipment lifecycle: specification, integration, commissioning, training, and ongoing support. A line may look efficient during a demonstration yet struggle with variable product sizes or frequent changeovers. Ask for measurable evidence, such as cycle time, repeatability, expected downtime, and recovery procedures. Check how systems communicate with existing equipment, and clarify which party maintains software and documentation. These details are easy to overlook. The boundary between engineering and daily operations is not always clean, and early assumptions sometimes need revision.
Tips: Share real product samples, layout drawings, and shift patterns before requesting a proposal. Confirm service coverage, spare-part lead times, and operator training. Ask what happens after a sensor fails at 2 a.m. A practical answer matters more than a polished demo.
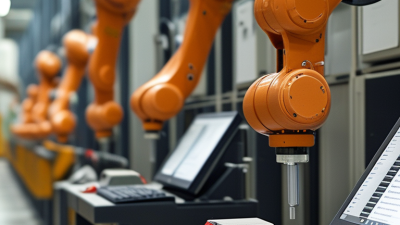
Automation engineering applies control systems, robotics, sensors, software, and industrial networks to operate and improve processes with reduced manual intervention. Its scope spans system design and integration, functional safety, commissioning, cybersecurity, and ongoing lifecycle support.
Regional shares of new industrial robot installations in 2023, rounded. The “Other regions” value is an approximate remainder. Source: International Federation of Robotics, World Robotics 2024. Regional adoption illustrates the global context in which automation engineering is designed and delivered.
Global automation systems are shifting from isolated machines toward connected, data-aware production cells. Industrial Ethernet and wireless links can carry sensor readings, alarms, and recipe changes across equipment. Edge computing processes time-sensitive signals near the machine, reducing dependence on distant servers. That matters when a conveyor must stop quickly after a safety sensor detects an obstruction. Machine vision is also becoming more adaptable, helping inspect surface defects, labels, and part orientation. Still, glare and changing materials can confuse a camera.
Digital twins let engineers test line layouts or control changes before applying them to physical equipment. They are useful only when models reflect real operating conditions; stale data can create false confidence. Collaborative robots can support repetitive loading and handling tasks alongside trained operators. Predictive maintenance combines vibration, temperature, and motor-current trends to flag wear before a breakdown. Cybersecurity and interoperability deserve equal attention: mixed-age machines rarely share data cleanly by default. Integration takes patience. Energy monitoring can reveal compressed-air leaks or idle motors, though savings depend on consistent follow-up. No single technology fixes a poorly designed process, and early deployments often expose assumptions teams missed.
Automation engineering in 2026 is shaped less by one universal blueprint than by local production needs.
In automotive and electronics plants, machine vision, collaborative robots, and traceable data systems help manage product variation. A camera inspecting a connector under changing light, for example, needs careful calibration, not just a faster processor. Small details matter. Food and packaging sites often prioritize washdown-ready equipment, quick changeovers, and reliable uptime across short production runs. Yet integration can lag: older controls and uneven network coverage still complicate otherwise capable systems.
In East Asia, dense supplier networks and export-oriented factories can support rapid deployment, especially where skilled integrators are available. North American buyers often weigh labor availability, retrofit costs, and cybersecurity alongside throughput when upgrading existing lines. Across Europe, energy use, machine safety, and flexible production frequently shape specifications, though priorities differ by sector and country.
In emerging manufacturing hubs, modular cells can offer a practical entry point where capital or maintenance skills are constrained.
Not a shortcut.
Buyers should verify cycle-time claims on representative parts, test recovery after faults, and confirm local service capacity before scaling. Regional patterns are useful, but they can hide differences between a coastal export plant and a smaller inland workshop.
That distinction deserves attention.
For global buyers, automation equipment should be judged against the work it must perform, not a polished brochure. Define the product range, target cycle time, changeover frequency, and operating environment before comparing offers. A quoted output rate may assume ideal materials and uninterrupted production. Ask how the system performs with your actual parts, operators, and shift pattern. Test it.
Integration deserves equal attention. Check whether controls, sensors, and data interfaces can communicate with existing equipment. Request layout drawings, utility requirements, and sample production records early; these reveal practical constraints before installation. Small details matter. Confirm which languages are available for operating instructions and service documents. Also verify applicable safety and documentation requirements in each destination market with qualified local professionals.
Purchase price alone gives an incomplete picture. Compare energy use, spare-part availability, training, maintenance intervals, and the cost of planned downtime over the equipment’s expected life. Ask who provides commissioning support, how quickly remote or on-site help can be arranged, and what response times are written into the service agreement. A tidy scorecard can still miss a messy plant floor. That is easy to overlook. Visit a reference installation where possible, and check that its materials and production demands resemble yours. Even careful evaluations leave uncertainty; record assumptions and open questions before signing.
| Automation Trend | What Buyers Should Evaluate | Practical Checks and Metrics | Recommended Evidence |
|---|---|---|---|
| AI-assisted operations and machine vision | Assess whether AI functions address a defined production task and can be monitored by operators. Check performance under representative product, lighting, and operating conditions. | Validate detection accuracy, false-reject and missed-detection rates, response time, and performance across test samples. Confirm how exceptions and model updates are handled. | Factory acceptance test results, sample test protocol, operating limits, update policy, and a clear manual fallback procedure. |
| Industrial connectivity and interoperability | Check whether the equipment can exchange required data with existing controllers, supervisory systems, and manufacturing software without unnecessary proprietary dependencies. | Verify supported protocols, data formats, interface availability, timestamp handling, and documented read/write permissions. OPC UA is one standardized option for industrial information exchange. | Interface and tag lists, network architecture, protocol documentation, and a witnessed integration test using the buyer’s intended systems. |
| Cybersecurity by design | Evaluate protection of equipment, credentials, remote access, and production data throughout installation and operation. Align requirements with the site’s security policies and risk assessment. | Check unique accounts, role-based access, secure configuration, patching process, backup and restore, network segmentation support, and remote-access controls. IEC 62443 provides a series of industrial automation and control system security standards. | Security architecture, account and access-control details, vulnerability and patch-handling process, and a documented remote-support procedure. |
| Energy-efficient and resource-aware automation | Compare energy and utility use in relation to actual production requirements, rather than relying on equipment ratings alone. Include compressed air and other relevant utilities where applicable. | Measure energy per good unit or production cycle at agreed operating conditions; record idle and standby consumption; identify measurement boundaries and relevant process variables. | Metered acceptance-test data, stated test conditions, utility connection requirements, and energy-management or shutdown settings. |
| Modular and flexible production systems | Determine how easily the equipment can accommodate product variants, changes in throughput, or future process steps without compromising safety or quality. | Review changeover time, supported product range, tooling requirements, capacity limits, recipe management, and the engineering work needed for a new configuration. | Changeover demonstration, configuration matrix, layout drawings, capacity assumptions, and documented scope for future modifications. |
| Predictive maintenance and condition monitoring | Check whether condition data helps maintenance teams identify actionable issues and whether alerts are understandable, timely, and relevant to the equipment. | Review monitored components, sensor coverage, alert thresholds, historical data access, false-alarm handling, and how recommendations are validated before maintenance action. | Example dashboards and alarm records, maintenance documentation, data-retention details, and a demonstration using representative operating data. |
| Digital engineering and virtual commissioning | Assess whether digital models and simulations support design review, control logic testing, operator training, or commissioning—and whether model assumptions match the delivered system. | Check model scope, data exchange formats, version control, simulation scenarios, and the process for reconciling the virtual model with the installed equipment. | Model deliverables list, simulation records, interface documentation, and agreed ownership and update responsibilities. |
| Functional safety and human-machine interaction | Confirm that hazards are assessed for the intended installation and that safety functions, access points, and operator tasks are addressed in the system design. | Review risk assessment, safety-function requirements, guarding, emergency stops, operating modes, and validation records. ISO 13849-1 and IEC 62061 are relevant standards for machinery safety-related control systems. | Risk assessment, safety-function specification, validation documentation, operating instructions, and site-specific integration responsibilities. |
| Lifecycle serviceability and total cost of ownership | Look beyond purchase price to installation, training, spare parts, maintenance, software support, downtime, and end-of-life requirements over the planned service period. | Compare warranty scope, spare-parts lead times, service response arrangements, maintainability, expected consumables, training needs, and support for software and components. | Itemized lifecycle-cost assumptions, maintenance schedule, spare-parts list, service-level terms, training plan, and support-period details. |
Buyer note: Compare proposals using the same product mix, operating conditions, acceptance criteria, data boundaries, and service assumptions. Verify applicable standards and regulatory requirements for the equipment’s destination and intended use.
Automation projects in 2026 should begin with the production problem, not the robot. The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023. That scale makes practical planning essential. Map cycle times, changeovers, and operator movements before selecting equipment. A pilot can look clean on paper and still struggle beside a dusty conveyor. Small pilots matter.
Integration deserves equal attention. Check whether new controls can exchange reliable data with existing machines, and define who owns alarms and downtime decisions. Deloitte’s 2024 Smart Manufacturing Survey found that 86% of manufacturing executives viewed smart manufacturing as a primary driver of competitiveness over the next five years. Yet connectivity alone does not deliver value. Teams need clear data rules, trained technicians, and realistic commissioning time. These details are easy to underestimate.
Safety and maintenance belong in the design review, not at handover. Assess access points, stopping behavior, and shared work zones with the people who use them daily. Plan for guarding, documented procedures, and safe troubleshooting. For maintenance, record baseline vibration, temperature, and cycle-time data, then set inspection intervals around actual operating conditions. Predictive alerts can help, but noisy readings still need human judgment. That part is imperfect, and worth reviewing.