China’s corrugated packaging industry has developed a strong base of Corrugated Roll manufacturers and suppliers. Their products support high-speed corrugators, stable flute formation, and consistent board quality. Yet supplier selection should involve more than price or catalog photographs.
Dr. David Roisum, a recognized converting and web-handling specialist, has emphasized, “Roll quality begins with control of surface, balance, and runout.” This principle applies directly to every Corrugated Roll used in demanding production environments. A polished roll surface can reduce paper marking. Accurate runout control can limit vibration at higher operating speeds. Proper metallurgy and heat treatment may also improve service life.
Details matter.
This guide examines Chinese suppliers through practical criteria, including manufacturing experience, flute specifications, steel quality, coating technology, dynamic balancing, and after-sales support. It also considers whether a supplier can provide inspection records, dimensional reports, and realistic delivery information. These documents are more useful than broad promises.
Some manufacturers appear highly capable, but available information is not always complete. That limitation deserves attention. Buyers should verify production facilities, technical drawings, tolerances, and testing procedures before making a final decision. A supplier with attractive pricing may still create hidden costs through premature wear, uneven pressure, or repeated installation adjustments.
The companies discussed here represent different capabilities and market positions. They should not be judged by marketing language alone. Actual performance depends on machine compatibility, operating conditions, paper grades, maintenance quality, and installation accuracy. This overview aims to provide a practical starting point for identifying reliable China Corrugated Roll manufacturers and suppliers.
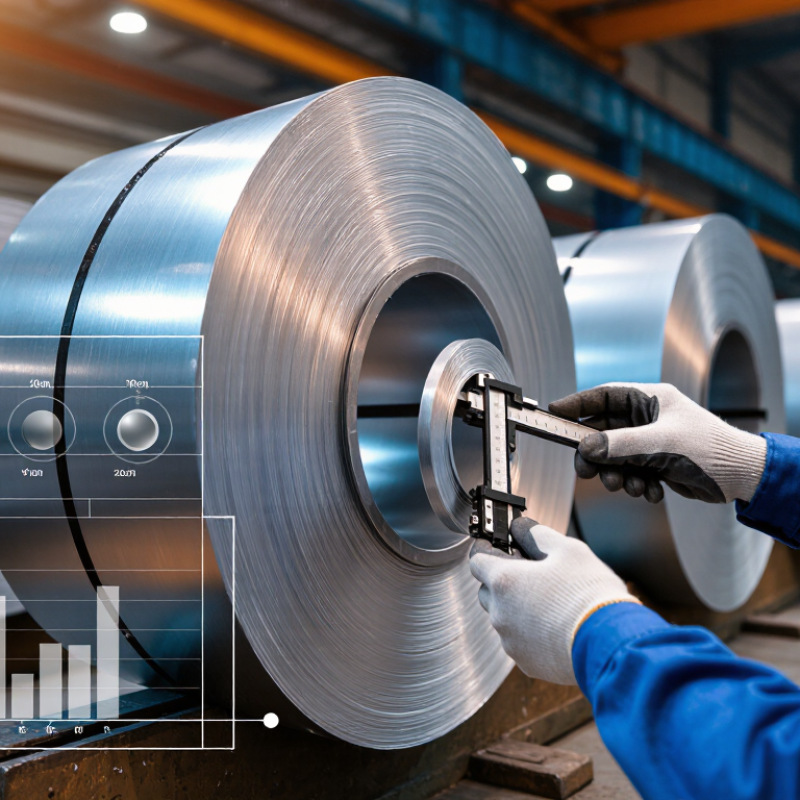
Corrugated rolls are precision-machined rollers used to form flutes in corrugated cardboard. Their heated surfaces press a paper liner into a wave-shaped profile. Adhesive then bonds this fluted medium between flat liners. The result is a lightweight board with useful strength and cushioning.
These rolls operate inside corrugating machines. Their flute profile controls board thickness, compression resistance, and printing performance. Smaller flutes suit retail cartons and detailed graphics. Larger flutes provide more cushioning for heavier products. Roll surfaces must maintain accurate gaps, stable temperature, and consistent pressure during continuous production.
A simple definition can be misleading. Corrugated rolls are not ordinary metal cylinders. Their tooth shape, hardness, coating, and alignment affect waste levels and board quality. Experienced manufacturers and suppliers usually discuss flute type, operating speed, paper grades, and machine dimensions before recommending a roll. Regular cleaning helps prevent adhesive buildup and uneven forming. Small alignment errors matter.
Selection still requires practical judgment. A roll that performs well on recycled paper may behave differently with lightweight kraft paper. Testing under real production conditions is more reliable than depending on a catalog specification alone. Wear also develops gradually, so maintenance records and measured flute profiles deserve attention.
China’s corrugated rolls are manufactured through a controlled sequence of machining, heat treatment, and precision inspection. Production usually begins with certified alloy steel selected for hardness, strength, and resistance to repeated pressure. Engineers calculate flute profiles according to board requirements, including flute height, pitch, and compression behavior.
The steel blank is turned on a CNC machine, then flute grooves are formed with specialized milling equipment. Heat treatment follows. It improves surface durability, but uneven heating can create distortion.
Manufacturers correct this risk through stress relief, hardness testing, and repeated grinding. The finished roll is polished to achieve a consistent surface.
Dynamic balancing is also essential because vibration can damage bearings and reduce production stability. Dimensional checks commonly examine flute accuracy, runout, surface roughness, and journal alignment.
A perfect result is not automatic. Small errors may still appear during installation or transport.
Tips: Ask for inspection records, hardness ranges, balancing results, and flute measurements before approval. Confirm the roll’s working width and machine compatibility. Trial testing with actual paper is valuable. Paper behavior can reveal problems that instruments miss. Keep storage areas dry, because moisture and careless handling may affect precision surfaces. Clear technical drawings also prevent avoidable misunderstandings between engineers and suppliers.
China Top Corrugated Roll Manufacturers and Suppliers
Key Types, Materials, and Specifications of Corrugated Rolls
Corrugated rolls shape the flute profile inside a single facer. Common profiles include B, C, E, and F flutes. Their heights typically range from 0.8 to 4.0 millimeters. BC and EB combinations support heavier double-wall packaging. Roll selection affects compression strength, paper consumption, and production speed. Small details matter.
Most industrial rolls use forged alloy steel cores. Their working surfaces may receive chrome plating or tungsten carbide coating. These treatments improve wear resistance and maintain flute accuracy. A practical specification should list roll diameter, face width, flute pitch, flute height, surface hardness, and allowable runout. Thermal control also deserves attention. Uneven heating can create unstable flute formation across a wide sheet.
Smithers reported that the global corrugated packaging market reached about 205 billion US dollars in 2023. Its forecast expects continued growth through 2028, increasing pressure on equipment efficiency. FEFCO industry statistics also show Europe producing tens of billions of square meters of corrugated board annually. This scale makes repeatable roll performance commercially important. Suppliers should provide inspection records, balancing data, and coating thickness results. Yet, one specification rarely fits every mill. Paper weight, recycled fiber content, steam pressure, and line speed can change the result. A cheaper roll may appear efficient, but early wear can increase waste and downtime. Testing remains necessary.
| Corrugated Roll Type | Primary Function | Common Flute Profile | Typical Roll Material | Surface Treatment | Typical Working Width | Typical Roll Diameter | Typical Hardness | Recommended Use |
|---|---|---|---|---|---|---|---|---|
| Single-Facer Corrugating Roll | Forms flutes in the medium and bonds the medium to a liner. | A, B, C, E, F, or customized profiles | Alloy steel, commonly heat-treated forged steel | Tungsten carbide coating, chrome plating, or other wear-resistant treatment | 1,600–2,800 mm | 280–450 mm | Approximately 58–70 HRC on the working surface, depending on coating | Single-face corrugators for standard, fine, and specialty board production |
| Double-Facer Corrugating Roll | Supports board bonding and maintains pressure while the corrugated web passes through the hot plate section. | Usually matched to the selected board flute | Heat-treated alloy steel or hardened steel | Chrome-plated, carbide-coated, or polished working surface | 1,600–2,800 mm | 180–300 mm | Approximately 50–62 HRC | Double-wall and multi-layer corrugated board lines |
| Pressure Roll | Applies controlled pressure to improve contact between the liner, adhesive, and fluted medium. | Plain cylindrical surface | Carbon steel, alloy steel, or ductile iron with a steel shell | Chrome plating, rubber covering, or polyurethane covering | 1,600–2,800 mm | 200–500 mm | Steel surface commonly 45–60 HRC; rubber hardness selected by process | Single-facer bonding and pressure-control assemblies |
| Glue Roll | Transfers a controlled adhesive film onto the flute tips before liner bonding. | Plain, grooved, or engraved metering surface | Stainless steel, chrome-plated steel, or hardened alloy steel | Hard chrome, ceramic, or polished stainless-steel finish | 1,600–2,800 mm | 180–300 mm | Approximately 45–65 HRC, depending on surface treatment | Starch adhesive application and high-speed single-facer systems |
| Metering Roll | Regulates adhesive thickness and stabilizes glue transfer to the applicator roll. | Fine engraved or precision-grooved surface | Stainless steel or hardened alloy steel | Chrome, ceramic, or other abrasion-resistant coating | 1,600–2,800 mm | 150–250 mm | Approximately 50–65 HRC | Precise adhesive metering for high-speed corrugating lines |
| Preheater Roll | Heats and conditions the liner or medium to improve moisture control and bonding performance. | Plain cylindrical surface | Carbon steel or alloy steel with an internally heated shell | Polished steel, chrome plating, or corrosion-resistant coating | 1,600–2,800 mm | 800–1,500 mm | Typically 35–55 HRC, depending on construction | Paper preheating, moisture balancing, and warp control |
| Lead-Out or Pull Roll | Guides and transports the corrugated sheet while maintaining web tension and alignment. | Plain, grooved, or rubber-covered surface | Steel core with rubber or polyurethane covering | Rubber, polyurethane, chrome, or textured elastomer covering | 1,600–2,800 mm | 250–500 mm | Elastomer hardness commonly 70–95 Shore A | Web handling, sheet transfer, and downstream converting sections |
| Flute Profile | Approximate Flute Height | Approximate Flute Pitch | Typical Flutes per 300 mm | Board Characteristics | Typical Packaging Applications |
|---|---|---|---|---|---|
| A Flute | Approximately 4.5–5.0 mm | Approximately 8.0–9.5 mm | Approximately 32–38 | High cushioning, good compression resistance, and strong stacking performance | Heavy-duty shipping cartons, protective packaging, and fragile products |
| B Flute | Approximately 2.5–3.0 mm | Approximately 5.5–6.5 mm | Approximately 46–55 | Good puncture resistance, flatter surface, and improved printability | Retail packaging, die-cut cartons, canned goods, and food packaging |
| C Flute | Approximately 3.5–4.0 mm | Approximately 6.8–7.9 mm | Approximately 38–44 | Balanced cushioning, compression strength, and material efficiency | General shipping cases, e-commerce cartons, and household products |
| E Flute | Approximately 1.0–1.8 mm | Approximately 3.0–3.5 mm | Approximately 85–100 | Fine surface, good folding performance, and high-quality printability | Consumer packaging, cosmetic cartons, food cartons, and small retail boxes |
| F Flute | Approximately 0.6–0.9 mm | Approximately 2.0–2.4 mm | Approximately 125–150 | Very fine flute structure, smooth print surface, and compact board thickness | Premium retail packaging, presentation boxes, and lightweight folding cartons |
| Double-Wall Combination | Combined height depends on flute pairing, such as BC or AB | Determined by the two flute profiles | Varies by combination | Higher rigidity, puncture resistance, and stacking strength than single-wall board | Export cartons, appliances, furniture, industrial parts, and heavy products |
| Specification Category | Recommended Data to Confirm | Typical Requirement or Reference Range | Why It Matters |
|---|---|---|---|
| Dimensional Accuracy | Outer diameter, working width, journal diameter, and total length | Defined by the machine model and flute profile; drawing-based production is preferred | Ensures compatibility with bearings, pressure settings, and the corrugator frame |
| Flute Geometry | Flute height, pitch, radius, symmetry, and flute count | Must match the required A, B, C, E, F, or customized profile | Controls board thickness, compression performance, paper consumption, and print quality |
| Surface Hardness | Hardness of the roll body or applied coating | Commonly about 50–70 HRC for hardened or coated working surfaces | Higher wear resistance supports longer service life and stable flute geometry |
| Surface Roughness | Working-surface roughness and polishing condition | Specified according to roll type, adhesive system, and paper grade | Affects paper traction, adhesive transfer, release behavior, and board appearance |
| Runout and Balance | Radial runout, dynamic balance, and journal concentricity | Set according to operating speed and equipment manufacturer requirements | Minimizes vibration, uneven pressure, noise, and premature bearing wear |
| Material and Heat Treatment | Steel grade, forging method, quenching, tempering, and case treatment | Forged alloy steel and controlled heat treatment are widely used for corrugating rolls | Provides the required strength, dimensional stability, and resistance to thermal cycling |
| Coating Thickness | Coating type, thickness, adhesion, and repair allowance | Varies by carbide, chrome, ceramic, or other engineered coating system | Determines wear resistance, corrosion protection, friction behavior, and maintenance options |
| Operating Temperature | Steam temperature, heating method, cooling arrangement, and thermal expansion allowance | Must be matched to the corrugator design and the selected roll construction | Reduces distortion and helps maintain consistent flute formation and bonding quality |
| Paper Compatibility | Basis weight, moisture content, liner grade, and medium grade | Common corrugating papers range from lightweight grades to heavy liner and medium stocks | Helps select flute geometry, pressure, coating, and roll surface characteristics |
| Maintenance Requirements | Cleaning method, lubrication points, inspection interval, and regrinding allowance | Follow the equipment manual and inspect for coating wear, scoring, deposits, and runout | Regular maintenance preserves roll accuracy, production speed, and board quality |
China’s leading corrugated roll manufacturers and suppliers serve packaging plants across many markets. Their products include corrugating rolls, pressure rolls, glue rolls, and cutting rolls. Smithers’ 2024 industry report valued the global corrugated packaging market at about US$176.6 billion. It forecasts growth to approximately US$205.8 billion by 2029. This expansion increases demand for stable, long-life roll systems.
Experienced Chinese manufacturers typically use alloy steel, controlled heat treatment, precision grinding, and dynamic balancing. Surface hardness matters because it affects wear, flute accuracy, and production stability. Buyers should request hardness records, runout measurements, balancing results, and material certificates. ISO-certified production can support reliability, but certification alone proves little without recent inspection evidence. Factory audits, sample testing, and clear after-sales procedures remain essential.
Tips: Compare flute profile, working width, line speed, coating method, and expected service hours. Ask suppliers for test reports from similar machines. Check packaging quality before shipment. Small details matter. A supplier may promise long service life, yet operating conditions often change the result. Humidity, paper quality, pressure settings, and maintenance habits can shorten roll performance. I have found that the cheapest quotation is rarely the lowest total cost. Still, even a premium specification can fail when installation support is weak. Request drawings, tolerances, replacement guidance, and response times in writing.
Selecting a Chinese corrugated roll supplier requires more than comparing online prices. Ask for material grades, hardness ranges, flute profiles, runout tolerances, and balancing records. A reliable supplier should explain how steel, coating, machining, and final inspection are controlled. Request recent inspection reports, not only polished photographs. During a video call, ask the engineer to show measuring tools and production flow. Small details matter.
A sample roll can reveal more than a sales presentation. Check surface finish under direct light, edge treatment, shaft dimensions, and packaging protection. If possible, test it on your own corrugator at normal speed with standard paper grades. Record vibration, adhesive behavior, flute consistency, and wear after a defined production run. Ask for a written acceptance standard. It prevents vague disputes. Confirm production capacity, lead time, replacement-part support, and response times in writing. Verify export documents and applicable quality certifications independently.
Supplier evaluation should include a factory visit or independent audit. Speak with quality staff, not only the sales contact. Review calibration labels, nonconformance records, and corrective-action evidence. Contact two recent customers through verifiable business channels. A common mistake is trusting a perfect sample too quickly. Be cautious when every answer sounds perfect. Real factories usually admit a limitation. I prefer clear evidence over confident promises. Start with a controlled trial order and define payment milestones, warranty terms, and remedies before production begins. Reassess the supplier after delivery, because one successful sample does not prove stable long-term performance.

